 |


| Quantity: | |
|---|---|
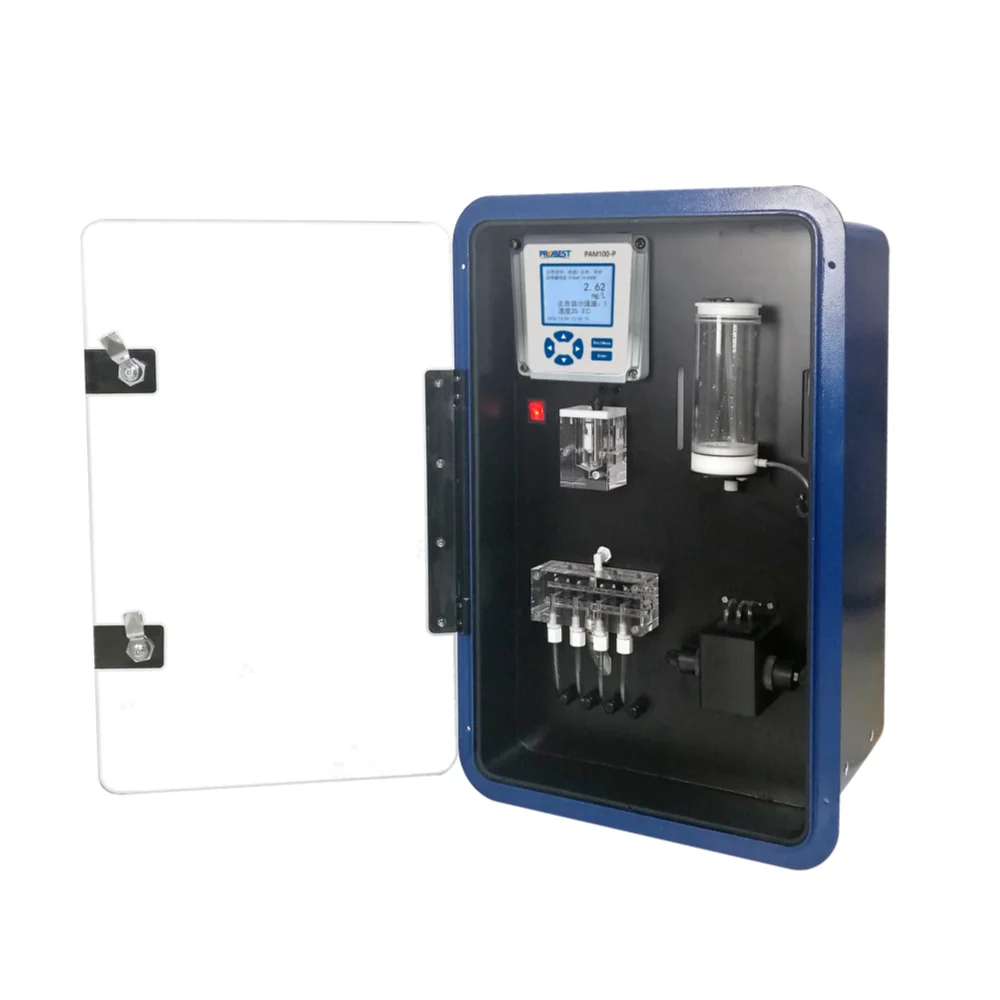
PAM100-P
PROBEST
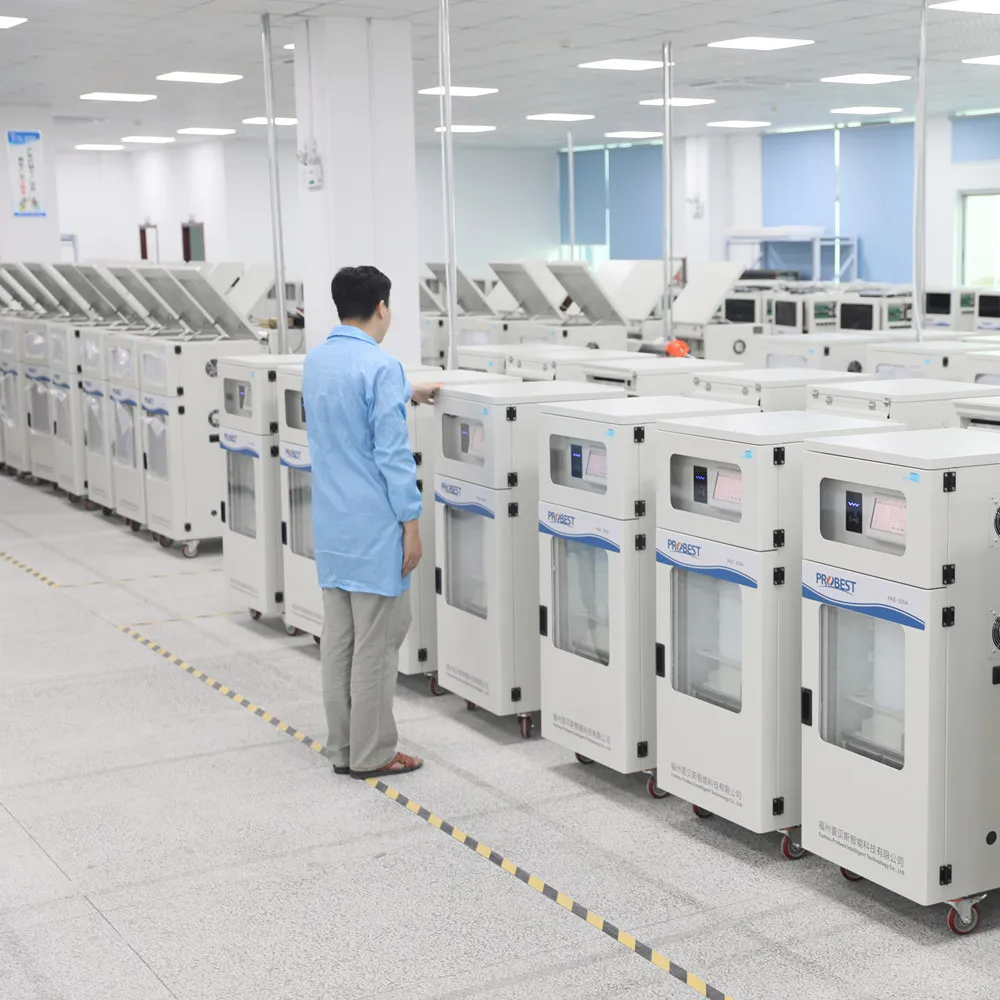
Warmly welcome online / on-site meeting with us to show you around our factory and know each other better.
Looking for OEM/ODM, or PROBEST Distributors Globally.
Join US ! Become Our Strategic Partners!
Our Highlights:
1. 50 R & D + 20 QA + 18 QC+ >200 employees.
2. ≥10 percent of annual turnover invested in R&D.
3.(RoHS/CE)hight quality + full tests before shipment.
4. >10000Square meter factory base.
5. Long service life, Low Maintenance.
Product Description
Measurement Principle
This instrument adopts the phosphorus vanadium molybdenum yellow photoelectric colorimetry. According to the Beer-Lambert Law, when a monochromatic light with corresponding wavelength passes through a colored solution, the light intensity will decrease because part of the light is absorbed by the light-absorbing particles in the solution. The relationship is as follows:
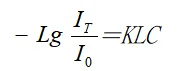
Where:
² IT is the transmitted light intensity,
² I0 is the incident light intensity,
² L is the liquid layer thickness,
² C is the solution concentration,
² K is a constant.
This is the Beer-Lambert Law, and the instrument analyzes and calculates the measured substance in the water sample based on the above formula.
Features
² Advanced embedded single-chip microcomputer technology;
² Compact structure, panel-mounted, full aluminum frame case, beautiful and sturdy, with strong anti-interference ability;
² Large dot-matrix liquid crystal display, intuitive and rich display content;
² Programmable 1-6 channels switching;
² Programmable modification of channel measurement cycle to effectively save reagents;
² With temperature measurement function, which can compensate measurement data according to temperature;
² Adopts imported light source and photocell, with long service life, small drift, stability and reliability;
² With black box function, which can query historical data, operation records and calibration records;
² Wide voltage (85~265VAC) and wide frequency (45~65 Hz), able to adapt to multiple conditions.
Applications
² In thermal power plants , real-time monitoring of phosphate concentration in boiler feed water and steam condensate to prevent scale formation caused by phosphates, which leads to reduced heat exchange efficiency or equipment corrosion.
² Monitoring phosphate concentration in circulating water or water supply systems in petrochemical, metallurgical and other industries to optimize the dosage of scale inhibitors and prevent pipeline blockage and equipment corrosion.
Technical Specifications
Measurement Range | (0-5) mg/L or (0-20) mg/L or (0-50) mg/L (specified when ordering) |
Instrument Indication Error | ±2% of full scale (F.S) |
Repeatability | No more than 1% |
Measurement Cycle | Programmable setting of 1-99 minutes, minimum 5 minutes |
Stability (Baseline Drift) | Using blank calibration, blank drift has no effect |
Stability (Chemical Drift) | ±1% F.S/24h (depending on reagent stability) |
Sample Conditions (Flow Rate) | (150-300) mL/min |
Sample Conditions (Temperature) | (5-50)℃ |
Allowed Solid Components in Water Sample | No more than 5 microns (no jelly-like substances allowed) |
Ambient Temperature | (5-45)℃ |
Ambient Humidity | No more than 90% RH (no condensation) |
Reagent Consumption | No more than 3 liters/30 days per type (1 type of reagent) |
Display | 320*240 dot-matrix liquid crystal, Chinese menu |
Isolated Output | (4-20) mA (isolated output, one per channel) |
Power Supply | AC (100-240) V, frequency (50/60) Hz or 24 VDC |
Power | 60 W |
Dimensions | 690 mm*450 mm*300 mm (height*length*depth) |
Cutout Size | 645 mm*410 mm |
Weight | 22 kg |
Why Choose PROBEST PAM100‑P On‑line Phosphate Monitor
PROBEST PAM100‑P phosphate online monitor is purpose‑built for continuous industrial phosphate water quality analysis. Compared with lab benchtop phosphate test kits, this on‑line phosphate detector delivers automatic 24‑7 running without frequent manual sample preparation. Multi‑channel function supports multiple water sampling points using single analyzer unit. Isolated 4‑20mA analog output connects to PLC, DCS and SCADA industrial control system for remote phosphate data acquisition. Widely deployed for power plant boiler phosphate monitoring, circulating cooling water phosphate control and semiconductor ultrapure‑water phosphorus contamination surveillance.
PRODUCT SHOW

ABOUT US


EXHIBITION

PRODUCTION PROCESS

CERTIFICATE


PACKAGE & SHIPMENT


